
Metal Injection Molding Manufacturer — MIM Parts & Services
Quick Answer
Metal injection molding services from Emitech combine metal powder and a polymer binder to produce complex, net-shape industrial metal components through injection molding, debinding, and sintering—not firearm parts. Our Nanjing facility supports the complete production chain from tooling design and material selection to surface treatment and quality inspection. Typical tolerances reach ±0.3%, part weights range from 0.1 g to 200 g, and standard lead times are 4–6 weeks after tooling approval—see our MIM cost guide and China MIM manufacturer page for detailed pricing and sourcing information. MIM is ideal for automotive sensors, surgical instruments, electronics hardware, and other small precision components produced in volumes from ten thousand to millions of units. First time learning about MIM? Start with What is MIM?
What Are Metal Injection Molding Services?
Metal injection molding, commonly called MIM, merges the design freedom of plastic injection molding with the strength of sintered metal. MIM parts start as a mixture of fine metal powder and a polymer binder. The feedstock is injected into a precision mold to form a green part, the binder is removed through debinding, and the brown part is sintered to 95–99% of theoretical density — a metal component with properties close to wrought equivalents, produced with little or no machining.
At Emitech, metal injection molding services cover the complete route from drawing to repeatable production: DFM review, mold build, feedstock compounding, molding, debinding, sintering, and secondary CNC machining where tighter features are needed — tolerances, traceability, and lead times under one accountable roof.

The Metal Injection Molding Process
Understanding the MIM process helps engineers specify parts correctly. Each stage affects final density, tolerances, and strength — and each has its own controls on our production floor.
| Step | What Happens | Key Controls |
|---|---|---|
| 1. Feedstock compounding | Fine metal powder (typically D90 ≤ 22 µm) is kneaded with a wax-polymer binder at roughly 60 vol% powder loading and granulated into pellets | Particle size distribution, powder loading, mix homogeneity |
| 2. Injection molding | Feedstock is injected into a hardened steel mold scaled up for sintering shrinkage, forming the oversized "green" part | Cavity shrinkage factor (15–20%), gate location, mold temperature, packing pressure |
| 3. Debinding | Binder is removed by solvent, catalytic, or thermal cycles, leaving a fragile "brown" part | Heating ramp, atmosphere, section thickness (thick walls debind slowly) |
| 4. Sintering | Brown parts are fired at roughly 1,100–1,400 °C in vacuum or hydrogen atmosphere; particles diffusion-bond and the part densifies to 95–99% of theoretical density | Temperature profile, atmosphere purity, setter support, shrinkage consistency |
| 5. Finishing & inspection | Optional sizing, machining, heat treatment, and surface treatment, then dimensional verification | CMM measurement, density and hardness checks, visual inspection |
Two points matter for designers. First, shrinkage of 15–20% linear sounds dramatic, but it is uniform and predictable: the mold cavity is scaled to compensate, which is why ±0.3–0.5% as-sintered tolerances are routine. Second, geometry is fully formed at the molding stage — complexity shows up in tooling cost, not unit cost.
Emitech MIM Production Capability
Emitech has worked in powder metallurgy since 1995 and has run MIM production since 2005. Feedstock, tooling, molding, debinding, sintering, sizing, and finishing are integrated at our Nanjing plant, supported by a 20+ person engineering team and an ISO 9001:2015 certified quality system:
| Production Area | Equipment on the Floor | Why It Matters |
|---|---|---|
| Injection molding | 17 MIM injection molding machines | Multi-cavity, multi-material scheduling without outsourcing |
| Debinding | 13 debinding furnaces (solvent, catalytic, thermal) | Cycle matched to binder system and section thickness |
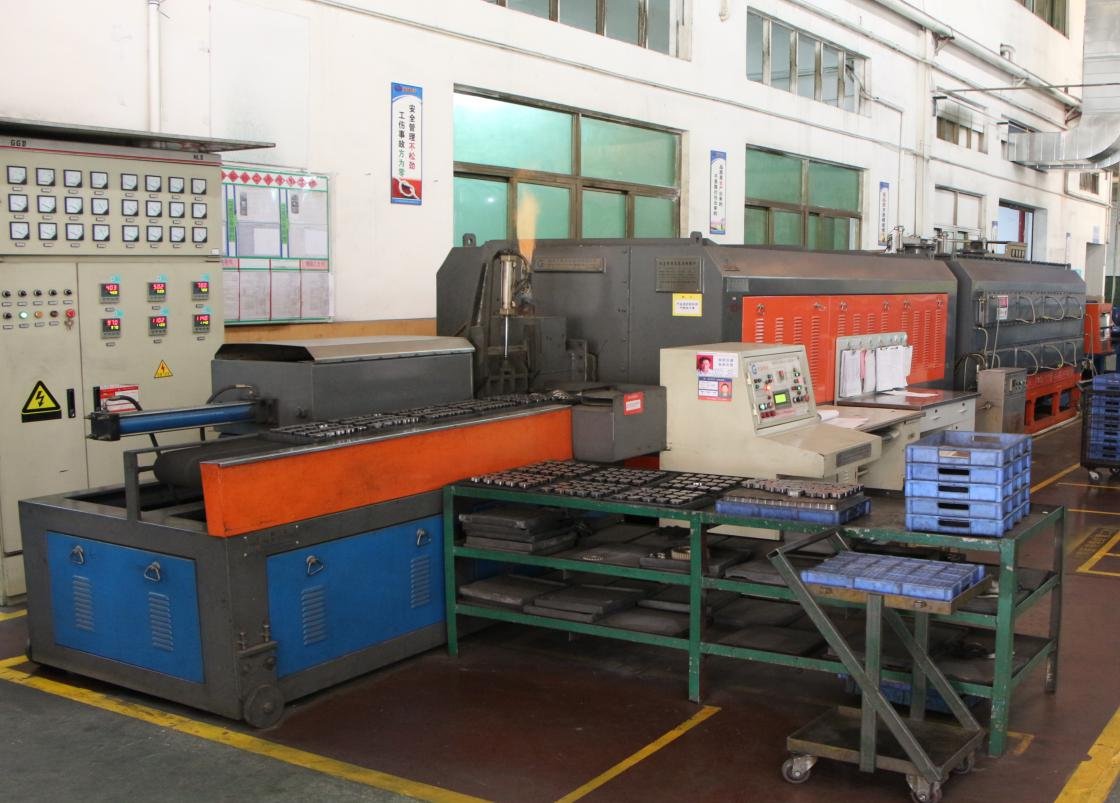
| Sintering | 4 continuous sintering furnaces (mesh-belt and pusher) plus 18 vacuum sintering furnaces | Volume carbon-controlled sintering, plus atmosphere-pure runs for stainless and titanium |
| Sizing & grinding | 24 sizing machines, 14 grinding machines, 27 presses from 6 T to 200 T | Coining and sizing for tolerances tighter than as-sintered |
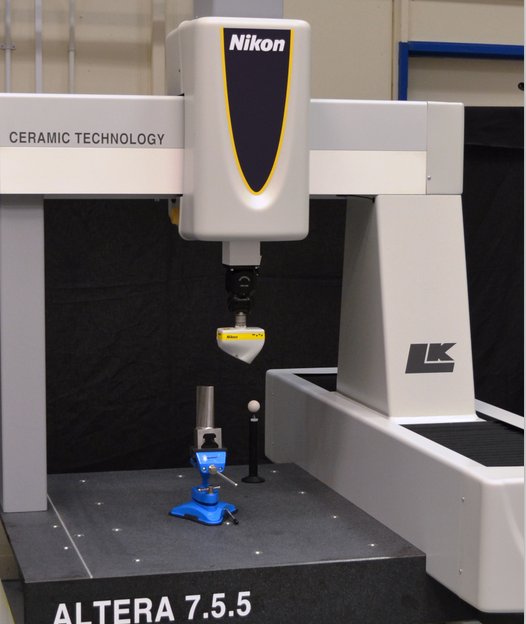
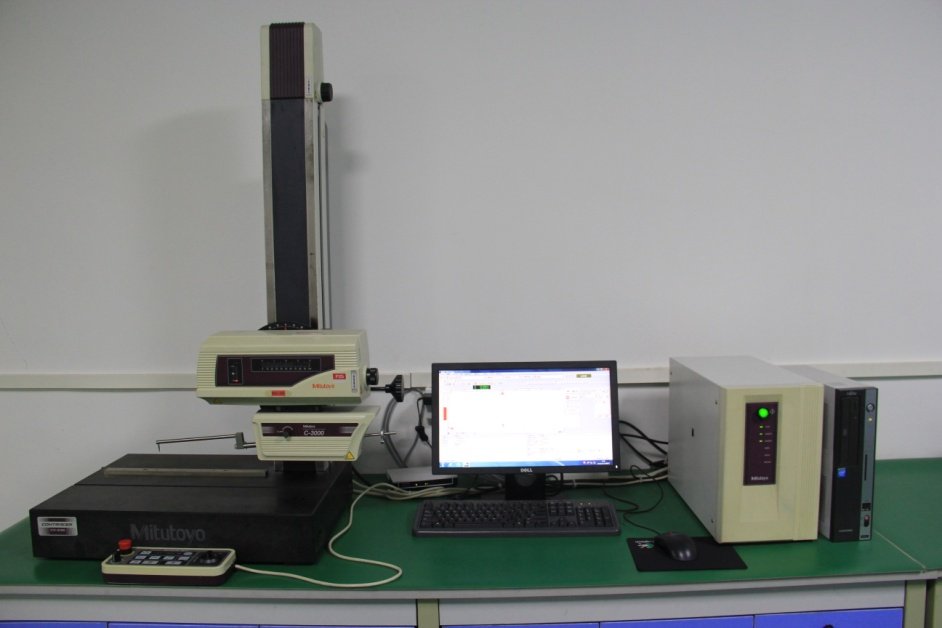
| Inspection & lab | Bridge CMM, optical vision projector, profilometer, roughness tester, universal testing machine, hardness testers, density meter, carbon-sulfur analyzer, magnetic particle testing, metallographic analysis | Critical dimensions and material properties verified before shipment |
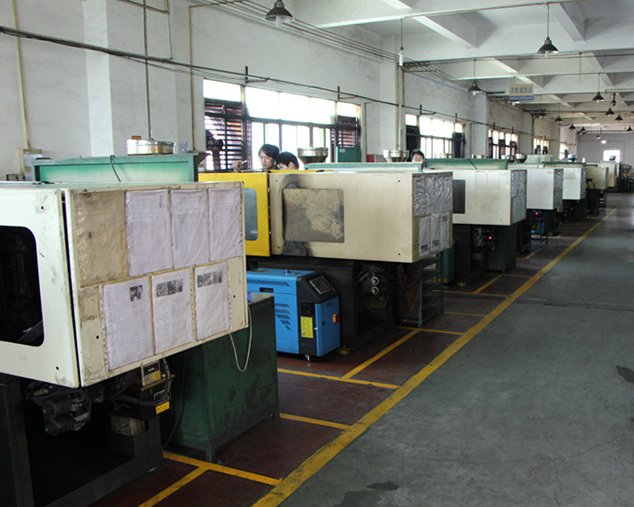
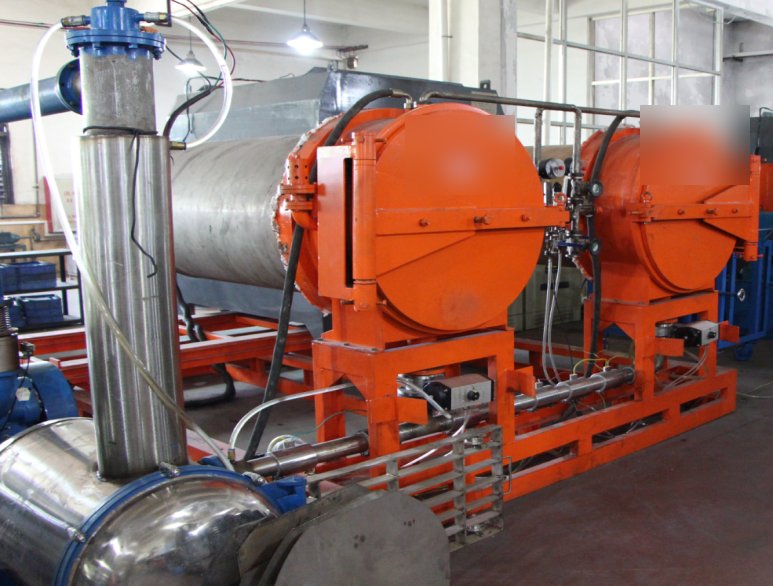
This is the capacity behind the figures buyers review: furnace throughput for stable monthly volumes, vacuum sintering for oxygen-sensitive alloys, and metrology that closes the loop on every lot.

MIM Materials and Applications
Almost any alloy that can be atomized and sintered can run through MIM — low-melting aluminum, zinc, and magnesium are the exception. Emitech processes more than 50 grades; typical values below are industry-published figures per MPIF Standard 35:
| Material Family | Common Grades | Typical Properties | Typical Applications |
|---|---|---|---|
| Austenitic stainless | 316L, 304L | ~520 MPa UTS, ~40% elongation (316L) | Corrosion-resistant housings, medical device components, fluid handling |
| PH stainless | 17-4PH (H900) | ~1,310 MPa UTS after aging | High-strength corrosion-resistant parts, aerospace, tools |
| Low-alloy steel | MIM-4605, 8620 | ~1,480 MPa UTS quenched & tempered (4605) | Gears, lock hardware, structural parts |
| Martensitic stainless | 420, 440C | Hardenable for wear and edge retention | Grinder burrs, blades, wear parts |
| Titanium | Ti-6Al-4V | ~900 MPa UTS, biocompatible | Medical and aerospace lightweight parts |
| Tungsten heavy alloy | 90–97W-Ni-Fe | Density 17–18.5 g/cm³ | Counterweights, radiation shielding |
| Soft magnetic | Fe-Si, Fe-Ni | Specified by magnetic performance | Sensor cores, solenoid and relay parts |
These are standard-published typicals, not best-case figures. On the Emitech floor, every lot is verified with density and hardness checks, plus carbon-sulfur analysis on carbon-sensitive grades. Grade-by-grade selection logic is in our MIM materials guide and material selection matrix.
MIM Standards: MPIF 35, ISO 22068, and ASTM B883
Three documents define MIM material quality language. MPIF Standard 35 (Materials Standards for Metal Injection Molded Parts) publishes the designations, chemistry, and minimum and typical mechanical properties of MIM grades — when we quote 316L or 4605, the referenced properties come from this standard. ISO 22068:2012 (Sintered-metal injection-moulded materials — Specifications) is the international counterpart. ASTM B883 defines chemistry and mechanical requirements for ferrous MIM materials in the ASTM system.
In practice: incoming powder is verified for chemistry and particle size; sintering atmospheres hold carbon and oxygen within grade limits; sintered density is measured per lot; and material certificates with heat-lot traceability ship with every order.
MIM vs CNC, Powder Metallurgy, Stamping, and Die Casting
MIM is the cheapest route when a part is small, complex, and needed in volume. The decision logic we apply during DFM review:
- Below ~10,000 parts/year, tooling rarely amortizes — CNC machining or 3D printing usually wins.
- Between ~10,000 and ~100,000 parts/year, MIM typically beats machining on unit cost for complex 3D geometry.
- Above ~100,000 parts/year, MIM is usually the lowest-cost route — 30–50% unit-cost reductions versus full machining are common, with ~95% material utilization instead of 50% or less from bar stock.
| Choose | When | Why |
|---|---|---|
| MIM | Small (0.1–200 g) complex steel, stainless, or titanium parts at 10k+ per year | Net-shape 3D geometry at the lowest unit cost |
| CNC machining | Volumes under ~10k/year, tolerances tighter than ±0.05 mm across the part, larger parts | No tooling investment; tightest tolerances; any size |
| Conventional powder metallurgy | Simple 2D shapes — gears, bushings — at very high volume | Cheaper tooling than MIM; limited to pressable geometry |
| Stamping | Flat or formed sheet-metal parts | Fast and cheap for sheet geometry; cannot form 3D features |
| Die casting | Larger parts in aluminum, zinc, or magnesium | Excellent for light alloys; cannot run steels or titanium |
Many Emitech programs combine both: MIM forms the net shape, then CNC finishes threads, sealing faces, and precision bores. Head-to-head detail: MIM vs CNC machining and MIM vs powder metallurgy.
Common MIM Production Issues and How We Control Them
Four issues account for most MIM production failures — and buyers should ask any supplier how they are controlled:
- Sintering distortion and slumping. Non-uniform walls shrink unevenly, and unsupported spans sag at sintering temperature. Prevention: uniform walls and a flat sintering datum at DFM, proper setters, controlled furnace profiles.
- Debinding cracks and blisters. Removing binder faster than it can diffuse out cracks thick sections. Cycle ramps are matched to the binder system and maximum section thickness.
- Carbon and oxygen pickup. A wrong furnace atmosphere embrittles or oxidizes parts. Vacuum or hydrogen atmospheres are selected per alloy, and carbon is verified by carbon-sulfur analysis.
- Porosity and density shortfall. Residual porosity cuts fatigue strength and corrosion resistance. Density is measured on every lot against the 95–99% theoretical window before parts ship.
Case Study: Telecom Cabinet Components — 50% Lighter, 50% Lower Cost
A leading global telecom equipment manufacturer engaged Emitech in an iterative redesign of cabinet hardware originally machined and fabricated from sheet metal. Converting the parts to MIM cut component weight by roughly 50% and unit cost by roughly 50%, while adding geometry freedom for compact enclosures.
The program has been in continuous mass production since 2015, and Emitech has since produced MIM components for 5G base station equipment at volume. (Customer name withheld under NDA.)
Case Study: Consumer and Lock Hardware in Serial Production
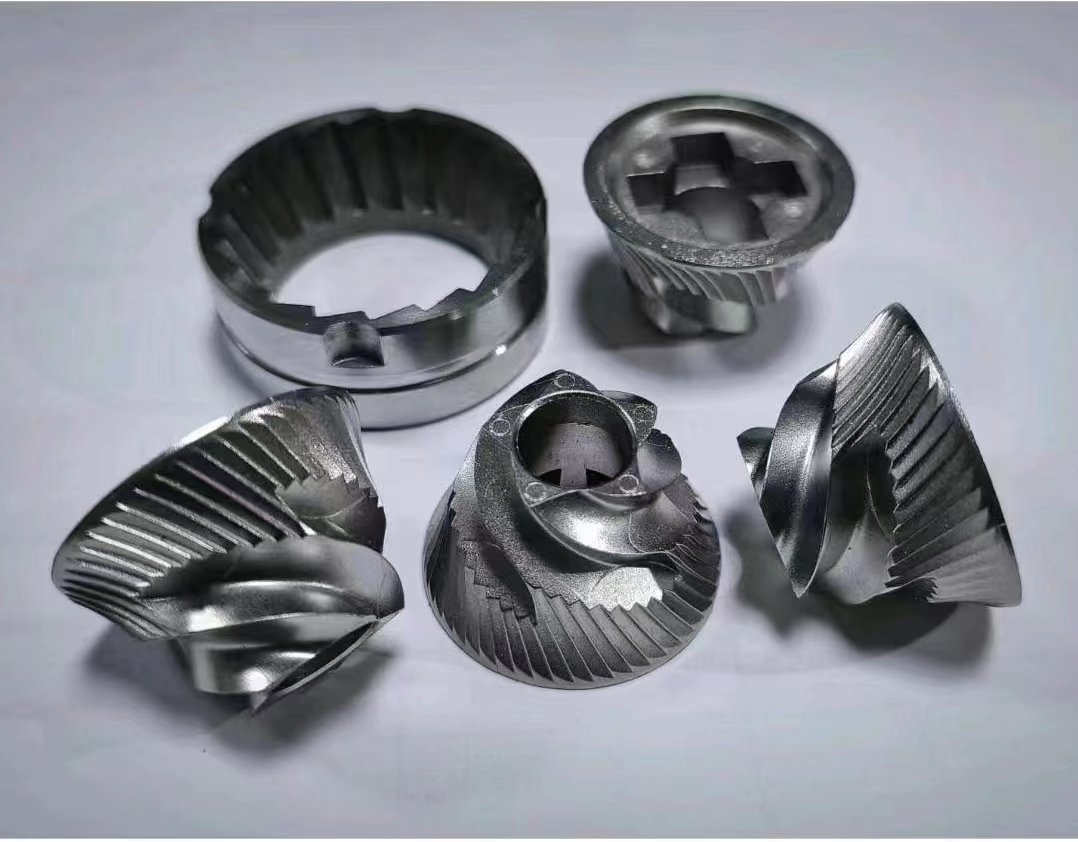
Coffee grinder burrs and grinding-disc sets are a long-running Emitech family, produced in series in 304, 420, and 316 stainless steel — 420 for hardness and edge retention, 304 and 316 for corrosion resistance and food contact.
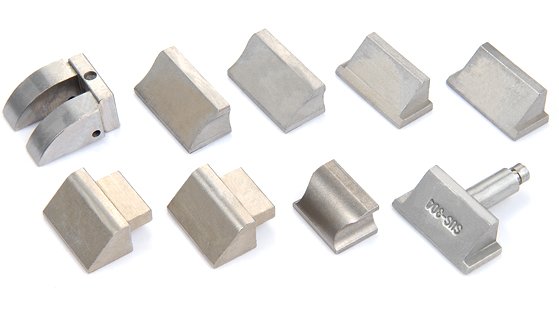
Lock hardware is a second staple: dead bolts, latch bolts, and lock cylinders molded net-shape, with serrations, cam profiles, and pin features formed in the tool. Both product families share one pattern — once the mold is qualified, MIM delivers high annual volumes of identical parts with no per-part machining. We also produce custom MIM parts for medical device components and other regulated applications.
Tolerances, Tooling, and Quality Assurance
Emitech's standard as-sintered MIM tolerance is ±0.3–0.5% of nominal dimension — for example ±0.15–0.25 mm on a 50 mm feature — with tighter features finished by sizing, coining, or in-house CNC machining. Wall thickness runs from 0.3 to 6 mm and part weights from 0.1 g to 200 g.
Molds are built in-house from H13, P20, and DC53 tool steels, with shrinkage compensation based on material-specific data accumulated across thousands of parts. MIM tooling lead time is typically 15–20 days for a single-cavity tool; complex multi-cavity molds are quoted case by case. For budgeting, see the MIM cost guide and typical MIM lead times.
Quality assurance is integrated into every step: incoming powder verification, green-part visual inspection, and post-sinter checks of density, hardness, and critical dimensions on our CMM and optical vision systems. First-article inspection reports, material certifications, and lot-level traceability from feedstock batch to shipment are standard — the process evidence medical device component and automotive programs require.

Industries Served by Emitech MIM


Emitech supplies metal injection molding services to automotive, medical, consumer electronics, industrial, and aerospace markets.
Automotive MIM Parts
Turbocharger components, sensor housings, fuel system parts, and ADAS hardware benefit from MIM's strength, repeatability, and cost efficiency at high volume.
Medical MIM Devices
Surgical instruments, orthopedic components, and dental tools in 316L, 17-4PH, and cobalt-chrome ASTM F75 with passivation and electropolish.
Consumer Electronics
Hinges, connectors, brackets, and watch hardware in stainless steel and titanium combine thin walls with premium surface finishes.
Industrial & Aerospace
Sensor cores, valve components, and lightweight brackets in specialty alloys for harsh operating environments.

Near-Net-Shape Efficiency: 95%+ Material Utilization
MIM is a near-net-shape process: the part comes out of the sintering furnace at final geometry, so almost every gram of powder becomes product. Material utilization exceeds 95%, versus machining from bar stock where 50–80% of the metal can end up as chips. Runner and reject material goes straight back into feedstock reprocessing within qualified recycling limits.
Frequently Asked Questions
Q: What is metal injection molding?
Metal injection molding (MIM) mixes fine metal powder with a polymer binder, injection molds the feedstock, then removes the binder and sinters the part to 95–99% of theoretical density. It produces small, complex metal parts in volume with properties close to wrought metal. Start with What is MIM?
Q: How does MIM compare to CNC machining?
MIM wins on small, complex parts above roughly 10,000 pieces per year: net shapes with ~95% material utilization and no per-part machining. CNC wins below that volume, on very tight tolerances, and on large parts. See MIM vs CNC machining.
Q: What materials can be used in MIM?
Most alloys that can be atomized and sintered: stainless steels (316L, 304, 17-4PH, 420, 440C), low-alloy steels (MIM-4605, 8620), titanium, soft magnetic alloys, and tungsten heavy alloys. Aluminum, zinc, and magnesium belong to die casting. See the MIM materials guide.
Q: What are typical MIM tolerances?
Typical as-sintered MIM tolerances are ±0.3–0.5% of the nominal dimension — for example ±0.15–0.25 mm on a 50 mm feature. Tighter features are finished by sizing, coining, or secondary CNC machining. Data by feature type is in our MIM tolerance guide.
Q: How much does MIM tooling cost, and when does it pay back?
A simple single-cavity MIM mold typically costs $3,000–$15,000; complex molds with side actions run $20,000–$50,000 or more. Tooling usually pays back from around 10,000 parts per year; above roughly 100,000 pieces annually MIM is typically the lowest-cost route. See the MIM cost guide.
Q: What is the minimum order quantity for MIM?
MIM is most economical at 10,000 parts per year or more because of the upfront tooling investment. Emitech also supports smaller validation and bridge-to-production batches — see our small batch MIM pricing guide.
Q: How do I get a MIM quote?
Send your 2D/3D drawing, material requirement, estimated annual volume, and quality specifications. Our engineers respond with DFM feedback plus tooling and unit pricing within 24 hours. Contact us to start.
Source Custom MIM Parts from Emitech
Nanjing Emitech delivers MIM from tooling through sintering and finishing. Custom MIM parts · MIM services · Request a quote · Email mim@mikeshoppingroom.com · WhatsApp +86 138 1403 4409
Why Buyers Choose Emitech for MIM Parts
With single-site production in Nanjing, we support global OEMs from prototype through mass production. Upload your 2D/3D drawings for a free design-for-manufacturability (DFM) review and quotation within 24 hours.
- Materials: 316L, 304, 17-4 PH, 4605, 8620, titanium, copper alloys, and custom feedstocks
- Industries: automotive sensors, medical instruments, industrial hardware, power tools, and electronics
- Quality: CMM inspection, density testing, and full traceability