🔥 What is a Sintering Furnace?
A specialized oven that heats powder compacts to50-80% of their melting point. This enables atomic diffusion without liquefaction.
Key Specs:1200°F - 3000°F | Controlled Atmosphere |97% Material Utilization.
Short version: the furnace is where a pressed or molded "green" part gains its final strength and density — the stage that decides whether a sintered metal part meets spec. How the machine works, what to control, and how furnace architecture maps to part cost and quality are covered below.
How Sintering Furnaces Work: The Fundamentals
The magic happens in a precise thermal window: high enough for atoms to move, but low enough to keep the part solid.
1. Atomic Migration
Atoms gain energy and migrate from their original positions to bond with neighbors. This happens1000x fasterat particle surfaces than in bulk material.
2. Neck Formation
As diffusion progresses, "necks" form between particles, pores shrink, and the powder compact solidifies into a dense, coherent part.

Temperature Control: The Master Variable
Precision is non-negotiable. A deviation of just 10-20°C can alter sintering kinetics significantly. Modern furnaces operate in three distinct ranges:
| Range | Temperature | Typical Materials |
|---|---|---|
| Low Temp | 1200 - 1800°F (650 - 980°C) | Bronze bearings, Simple Stainless |
| Medium Temp (Industry Standard) | 1800 - 2400°F (980 - 1315°C) | Automotive Parts, Iron-Copper-Carbon, Structural Steel |
| High Temp | 2400 - 3000°F (1315 - 1650°C) | Refractory Metals, Advanced Ceramics, Reactive Metals |
Atmosphere Control: Chemistry in the Oven
The atmosphere isn't just "air"—it's a chemical reactant. It removes oxides and controls carbon.
🔥 Reducing Atmospheres
Gases:Hydrogen, Dissociated Ammonia.
Function:Strips oxide layers off particles to expose clean metal for bonding. Essential for most metals.
🏭 Endothermic Gas
Gases:CO, H₂, N₂ (Burnt Natural Gas).
Function:The workhorse for steel. ControlsCarbon Potentialto prevent parts from losing hardness (decarburization).
🌌 Vacuum
Gases:None.
Function:For reactive metals (Titanium, Tungsten) that oxidize instantly in air. Also enables precise chemistry control.
Pro Tip:Modern systems use real-time Oxygen Sensors and Dewpoint Analyzers to adjust gas flow automatically.
Sintering Furnace Types: Selecting the Right Architecture
Your production volume and material sensitivity dictate the machine architecture. Use this comparison to select the right fit.
| Furnace Type | Temp Range | Atmosphere | Throughput | Best For |
|---|---|---|---|---|
| Batch | Up to 3000°F | All types | Low (10-1000 kg) | R&D, Dental, Custom Jobs |
| Continuous Belt | 1800-2600°F | Reducing / Endo | High (500 kg/hr) | Automotive High Volume |
| Pusher | 2200-3000°F | All types | Medium (200 kg/hr) | Heavy Parts, Ceramics |
| Vacuum | Up to 3000°F | Vacuum / Inert | Batch (5-500 kg) | Reactive Metals (Ti), Tool Steel |
| Walking Beam | 1800-2800°F | Reducing / Endo | Very High (1000 kg/hr) | Massive Volume (Conn Rods) |
🏭 Continuous Belt (The Workhorse)
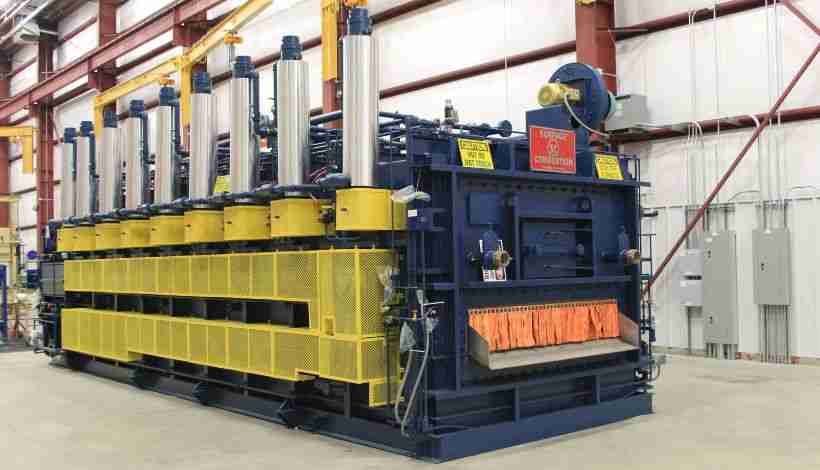
Parts move on a mesh belt through zones. Once stabilized, it runs continuously with minimal intervention. Standard for small-to-medium automotive parts.
🌌 Vacuum (The Specialist)
Essential for reactive metals (Titanium) or tool steels requiring gas quenching. High cost, but zero contamination.
🧱 Pusher (The Heavy Lifter)
Advances trays mechanically. Best for heavy loads or high temps where belts would fail (Ceramics, Refractory).
Material-Specific Applications
1. Low-Alloy Steel (Automotive)
Largest Application.Gears, sprockets, pulleys. Net-shape capability with >97% material utilization eliminates machining.
2. Technical Ceramics
Alumina & Zirconia. Cannot be melted (too high Tm). Sintering is theonlyviable route for cutting tools and implants.
3. Cermets (WC-Co)
Liquid Phase Sintering.Hard carbide particles bonded by a cobalt matrix. Impossible to produce via melting due to incompatible melting points.
4. Additive Manufacturing (Binder Jet)
The furnace is the engine of Metal AM. It debinds the printed polymer and densifies the remaining metal skeleton.
Critical Process Variables
Part quality depends on balancing these four interdependent factors:
Troubleshooting: Sintering Defects
Identify the symptom to find the process fix.
⚠️ Dimensional Distortion
Cause:Non-uniform green density or thermal gradients.
⚠️ Surface Oxidation
Cause:Poor atmosphere control, air leaks, or wet gas.
⚠️ Inadequate Density
Cause:Low temp, short time, or sensor error.
⚠️ Excessive Grain Growth
Cause:Overheating or holding too long.
Video: Animated demonstration of atomic diffusion without melting.
Sintering Parameters by Material Category
Optimal properties require specific Time-Temperature-Atmosphere combinations. Use these baselines for process development.
| Material System | Temp (°C / °F) | Hold Time | Atmosphere | Target Density |
|---|---|---|---|---|
| STEEL & IRON ALLOYS | ||||
| Ferrous PM(Fe-Cu-C) | 1120°C(2050°F) | 20-40 min | Endothermic | 90-93% |
| Sinter-Hardening | 1260°C(2300°F) | 25-35 min | Endo + Fast Cool | 92-95% |
| SS 316L | 1300°C(2370°F) | 60-90 min | H₂ / Vacuum | 94-97% |
| NON-FERROUS & CARBIDES | ||||
| Bronze(Cu-Sn) | 845°C(1550°F) | 10-20 min | DA (NH₃) | 88-92% |
| Titanium | 1250°C(2280°F) | 120-240 min | Vacuum (High) | 97-99% |
| Tungsten Carbide | 1400°C(2550°F) | 30-60 min | Vacuum / H₂ | 98-99.5% |
| ADVANCED CERAMICS | ||||
| Alumina(Al₂O₃) | 1600°C(2910°F) | 120-180 min | Air | 96-99% |
| Silicon Nitride | 1700°C(3090°F) | 60-120 min | Nitrogen | 97-99% |
Advances in Sintering Technology
Modern furnaces are smarter and more efficient. Three key innovations driving the industry:
💻 1. Adaptive Process Control
The Tech:Real-time sensors + Adaptive algorithms.
The Benefit:Automatically adjusts heating profiles based on actual thermal response. Predictive maintenance prevents surprise failures.
⚡ 2. Energy Efficiency
The Tech:Ceramic fiber insulation & Heat recovery systems.
The Benefit:Reduces heat loss significantly. Waste heat preheats incoming parts, cutting energy bills.
🔬 3. Atmosphere Management
The Tech:Laser-based gas analyzers & Mass spectrometry.
The Benefit:Precise, closed-loop control of Carbon Potential and Dewpoint. Essential for high-performance alloys.
Selecting Your Furnace: A Buyer's Checklist
Match the machine to your mission. Don't overbuy or under-spec.
Do you need 1120°C (Steel) or 1600°C (Ceramics)? Does your material require Vacuum, or is cheap Endothermic gas sufficient?
<100 kg/day:Batch Furnace (Flexibility).>200 kg/day:Continuous Belt (Efficiency). Don't buy a continuous line for R&D.
Metallic elements work up to 1300°C. Above that, you need Graphite or Molybdenum (Expensive). Factor replacement cost into ROI.
Do you need "Sinter-Hardening" (Rapid gas quench)? Standard furnaces cool slowly; hardening furnaces cool fast to lock in martensite.
Frequently Asked Questions
Q: What is the operating temperature range?
1200°F - 3000°F (650°C - 1650°C). Specifically 50-80% of the material's absolute melting point (Sub-solidus).
Q: How long does a cycle take?
A Batch Furnace takes 2 - 8 Hours (Full cycle). A Continuous Belt takes 30 Mins - 2 Hours (Transit time). Rapid Sintering takes < 2 Hours (Dental Zirconia).
Q: What is the difference between Sintering and Annealing?
Sintering creates the part. It consolidates loose powder into a dense solid body via atomic bonding. It fundamentally changes the state (Powder → Solid). Annealing modifies the part. It is a heat treatment applied to an existing solid to relieve stress or soften microstructure. No consolidation occurs.
Q: Why is atmosphere control critical?
To remove oxides. Oxide films block atomic bonding. Reducing atmospheres (H₂, CO) chemically strip these oxides, exposing clean metal for diffusion. Without this, you get zero strength.
Q: What determines final density?
It is a multivariate equation including green density, temperature, time, and powder size. The goal is to balance densification against grain growth to hit 85-99% theoretical density.
Q: How do you prevent distortion?
Uniformity is key. Ensure uniform green density (pressing) and uniform thermal exposure (furnace). Use support fixtures for complex geometries to prevent gravity sagging.
Q: What are the main types of sintering furnaces?
The four architectures in production use are batch vacuum furnaces, continuous (mesh-belt or pusher) furnaces, walking-beam furnaces, and batch atmosphere (hump-back or box) furnaces. Vacuum batch furnaces dominate MIM and stainless work because they remove oxygen and binder residue without leaving carbon control to a generated atmosphere; continuous furnaces win on cost per part once volumes justify the line. Our MIM sintering furnace walkthrough covers how each type fits a powder metallurgy production flow.
Q: How much does a sintering furnace cost?
Pricing is quoted per configuration, so treat any single number with care: the drivers are hot-zone size, maximum temperature, atmosphere system (vacuum pumps versus generated hydrogen/nitrogen), and automation level. A laboratory batch unit and a production continuous line sit in entirely different budget classes. For MIM parts buyers the more useful question is process cost per kilogram of parts — the furnace specification is your supplier's problem, and you verify it through their process capability, not through the equipment price tag. Request a MIM parts quote and the process window (temperature, atmosphere, furnace type) is documented alongside the part.
Q: Batch or continuous furnace — which one makes my parts?
Volume decides. Continuous mesh-belt and pusher furnaces run one to three shifts of steady throughput and lowest cost per part, but they fix the atmosphere, profile, and belt temperature ceiling — fine for iron, copper, and some stainless, not for high-temperature MIM alloys. Batch vacuum furnaces swap profiles per load, reach the temperatures MIM stainless and tool steels need, and suit small-to-medium volumes at a higher cost per cycle. If your annual volume is in the hundreds of thousands of small parts, both routes can compete; ask which one your supplier runs and how profile uniformity is verified.
Q: What is a sintering furnace diagram likely to show?
The canonical diagram shows a cold entry (debind residue burnoff), a ramp-and-hold hot zone where atomic diffusion bonds the particles, and a controlled cooling exit — plus the atmosphere circuit (vacuum pumps or gas flow) that keeps oxygen out. For continuous furnaces the diagram stretches the same three stages into a belt path with multiple zones. The physics being illustrated is on our sintering explainer: neck formation between powder particles, then densification as pores close.
Conclusion: The Pillars of Success
Sintering furnaces are precision instruments that convert loose powder into high-strength components with97% material utilization. Success relies on three pillars:
1. Precision Control
Temperature uniformity (±5°C) and Atmosphere management (Dewpoint/Carbon Potential) are non-negotiable.
2. Proper Architecture
ChooseBatchfor flexibility (R&D),Continuous Beltfor volume (Auto), orVacuumfor reactivity (Titanium).
3. Material Match
Know your numbers: Steel needs 1120°C/Endo gas; Tungsten needs 2300°C/Hydrogen. The furnace must fit the physics.
Precision Metal Parts from Emitech
Nanjing Emitech delivers MIM, CNC machining, and custom metal parts. MIM services · Request a quote
Last updated: 2026-06-24
Continue reading
- MIM 440C: How High Hardness (HRC 58-60) Transforms Product Performance
- MIM 4605: A Comprehensive Analysis of Low-Alloy Steel Performance and Applications
- How MIM Auto Parts Reduce Costs and Improve Quality in the Automotive Industry
- Metal Injection Molding Design: How to Optimize Parts for Manufacturing